If you’ve ever walked the floor of a machine shop, or stood behind the glass of a CNC lathe operator’s booth watching a machine bite into a block of metal, you’ve probably noticed it does not work at the same pace the whole time. First it carves away big chunks of material, sometimes leaving shavings so thick they curl like autumn leaves, then it switches to a lighter, slower pass that leaves a surface so smooth you could run your thumb over it without catching. That split between fast, aggressive cuts and slow, precise ones is the heart of roughing and finishing in CNC lathe work. As a CNC lathe supplier, I get asked about this difference all the time—most of the time, it’s not enough for customers to just know “one is rough, one is fine”; they need to understand why both steps matter, how they work together, and how a well-built CNC lathe makes both tasks better. CNC Lathe
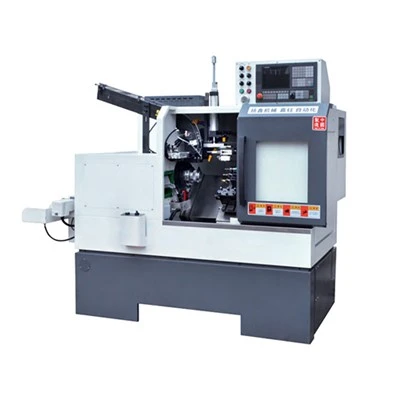
Let’s start with what roughing actually is. When a raw block of metal arrives at a shop, it’s almost always a little bigger than the final part needs to be. It might have leftover cast marks, excess material from forging, or just extra stock that needs to be removed. Roughing is the first step: the CNC lathe’s cutting tool plunges into the workpiece with a deep cut, sometimes taking thousands ofths of an inch of material off in a single pass. The goal here isn’t perfection—it’s speed. We want to remove as much excess material as possible in the least time, and that means prioritizing material removal rate over surface finish. To do that, roughing tools are usually tougher, more robust, and made to handle the extreme force of deep cuts. On a good CNC lathe, the spindle, ways, and tool turret are built to hold steady under that force—no vibration, no wobble—because if the machine shakes during roughing, you get a part that’s off-size, or a tool that snaps mid-cut and has to be replaced, wasting time and material.
But roughing has to leave enough material for the second step. That’s where finishing comes in. Once the bulk of the excess is gone, the workpiece is only a few thousandths of an inch away from its final shape and dimensions. Finishing cuts are shallow, precise, and slow. The tool takes very light passes, sometimes removing just a few tenths of a thousandth of an inch per pass, to carve the exact profile, create the surface finish the part requires, and hit tight dimensional tolerances—often within +/- 0.001 inches, or even tighter for medical or aerospace parts. The tools used for finishing are different too; they’re often sharp, polished, and made to produce a smooth edge, not to withstand heavy force. A lot of newer CNC lathes have separate toolholders for roughing and finishing, designed to hold each tool with perfect concentricity—so when the finishing tool spins, it doesn’t wobble, and every pass is consistent.
What surprises a lot of new machinists is that roughing and finishing aren’t just two random steps someone made up. They’re tied together by something called “stock allowance”—the amount of material left after roughing for finishing. If you leave too little, your finishing tool might dig into the hard, outer “skin” of the raw metal, or even cut away material that was already shaped during roughing, leading to a part that’s too small. If you leave too much, the finishing tool has to take too heavy a cut, which can cause chatter—that high-pitched vibration that leaves a rippled surface and ruins the finish. On older CNC lathes, setting the right stock allowance is a manual call the operator has to make, based on their experience. But on the models we supply, the control software can calculate that automatically, based on the workpiece material, tool type, and desired finish, taking the guesswork out of it.
Let’s talk about how each step affects the machine itself, because that’s where choosing the right CNC lathe makes all the difference. Roughing puts a lot of stress on every part of the machine. The spindle has to generate enough torque to turn the thick metal against the heavy cutting force. If a spindle is weak or poorly built, it will stall during roughing, or flex, leading to inconsistent cuts. The machine’s bed and ways have to be rigid enough to absorb that force, too—no flexing means every point on the workpiece is in the same position the whole time, so cuts are uniform. Finishing, on the other hand, demands precision. The spindle has to spin at consistent, often high speeds, and the tool turret has to index to exactly the right position, over and over, without any slop or play. If there’s even a tiny amount of backlash in the lead screw, a finishing cut will end up slightly off in diameter, which can make a part unusable for its intended application.
I see a lot of small shops try to skip steps, too, running a single cut that tries to do both roughing and finishing. For small, low-tolerance parts, that might work for a little while, but it costs them in the long run. A single cut for both means running at a compromise speed—too slow for roughing to be efficient, too shallow to get a good finish. A friend of mine runs a small precision parts shop; he told me he used to run every part in one pass to save time, but after upgrading to our series of CNC lathes, he split every job into roughing and finishing, and his overall throughput went up by 30%—because his roughing cuts were faster (thanks to the machine’s rigidity), and his finishing cuts were more consistent, so he had far fewer scrap parts.
Material choice also changes how roughing and finishing are done. For example, machining aluminum—soft, ductile, and easy to work with—lets you take deeper, faster roughing cuts, with a larger stock allowance for finishing. But aluminum is also prone to “built-up edge”: when tiny bits of melted metal stick to the cutting tool, leaving rough streaks on the part. That means finishing cuts on aluminum often require sharp tools and specific speeds to avoid that issue. Stainless steel, by contrast, is hard and abrasive, so roughing cuts have to be slower, with tools made to withstand heat, and the finishing step has to be precise to avoid work-hardening the surface of the part. Work-hardening happens when stainless steel is cut too aggressively after roughing; the surface gets harder, so the finishing tool can’t cut it smoothly, leading to a rough finish. A good CNC lathe will let you adjust feeds and speeds for both steps based on the material, and many of our models come with pre-loaded material profiles that make that adjustment automatic.
Another key difference is tool life. Roughing tools wear out much faster than finishing tools, because they’re taking bigger bites and dealing with more force, heat, and material. If a roughing tool starts to wear, it leaves an uneven stock allowance, which means the finishing tool has to work harder to compensate, leading to more wear on the finishing tools too. Monitoring tool life is critical for both steps—on our CNC lathes, the control system tracks how many hours each tool has been used, and sends an alert when it’s time to replace a roughing tool, so operators don’t end up with bad stock allowance that ruins a part. Finishing tools, because they’re working with light cuts, last much longer, but they have to be kept sharp at all times; a dull finishing tool will leave a grainy surface, no matter how precise the machine is.
What about when someone needs a high level of surface finish? For applications like automotive engine parts, medical implants, or aerospace components, a standard finishing cut might not be enough. Some jobs need a secondary finish step after the CNC lathe is done, like grinding or polishing, but a good CNC lathe can get you 90% of the way there with a fine finishing pass. The difference between a basic finish and a high-gloss finish often comes down to the feed rate of the finishing cut: a slower feed rate leaves smaller tool marks, so the surface is smoother. But that slower feed rate means the machine has to be perfectly rigid, with no vibration, otherwise the tool will chatter and leave those ripples. That’s where the quality of the CNC lathe’s construction shines through—cheap lathes might not hold up to slow, precise finishing cuts, so you have to do extra work post-machining, which adds time and cost.
I’ll be honest, when I first started working as a CNC lathe supplier, I thought the difference between roughing and finishing was just common sense. But over the years, I’ve seen customers who’ve spent years working with older machines struggle with scrap parts, long cycle times, and high tool costs, just because they didn’t fully understand how the two steps work together. For example, a customer last year had a job making small aluminum gears that kept coming out with uneven teeth. He was running a single cut, so his roughing cuts were too shallow, leaving him with not enough stock for finishing, and his finishing cuts were trying to take too heavy a bite. Once we adjusted his process to separate roughing and finishing, and set the right stock allowance on our CNC lathe, his scrap rate dropped from 15% to almost zero, and his cycle time per gear went down by 20%. That’s the kind of difference that understanding this basic concept makes.
Now, if you’re just getting started in machining, or looking to upgrade your CNC lathes, it’s important to ask questions about how a machine handles both roughing and finishing. Does it have a rigid spindle that can handle heavy roughing cuts? Does the tool turret hold tools with enough concentricity for precise finishing? Does the control software make it easy to set stock allowances and adjust feeds and speeds for different materials? These aren’t just technical details—they directly affect how much time and money you save, and how good your parts turn out.
Roughing and finishing aren’t two separate, disconnected steps—they’re part of a single, balanced process. Roughing removes the bulk of the material as fast as possible, without sacrificing part quality; finishing shapes that remaining material to exact dimensions and a smooth surface, without wasting time on unnecessary heavy cuts. A great CNC lathe doesn’t just execute either step well—it bridges them, making the transition smooth, consistent, and efficient. If you’re looking to upgrade your machining operations to reduce cycle times, lower scrap, or tackle more precise jobs, we can help you find the right CNC lathe for your specific needs. Contact our team to discuss your application, review process requirements, and find a solution that fits your production goals.
Horizontal Machining Center References
Groover, M. P. (2020). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems. Wiley.
Clark, E. (2018). CNC Lathe Operations and Programming. Industrial Press.
Kascak, A. F. (2015). Metal Cutting Theory and Practice. CRC Press.
Taizhou Qiyang Trading Co., Ltd.
As one of the most professional CNC lathe manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk CNC lathe for sale here and get quotation from our factory. Customized orders are welcome.
Address: Zhenhai Village, Binhai Town, Wenling City, Taizhou City, Zhejiang Province
E-mail: qycncmachine@outlook.com
WebSite: https://www.qycncmachine.com/
