If you’re a small business owner, a hobbyist, or a creative startup exploring resin 3D printers for low-volume production, one of the first questions you’re likely to ask is: “How fast does this thing actually work?” As a supplier of resin 3D printers, I hear this question at least a dozen times a week, and it’s not one with a one-size-fits-all answer. The truth is, resin 3D printer production speed depends on more than just the machine itself—everything from layer height to resin type, part complexity, and post-processing workflow plays a role. To help you make an informed choice, I’ll break down what you need to know about real-world production speeds for small-scale resin 3D printing, straight from the supplier’s perspective. Resin 3D Printer
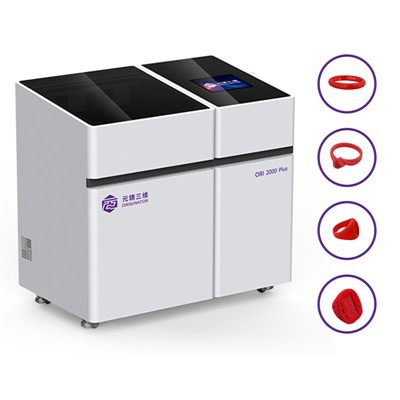
First, let’s set the context: small-scale production here means runs of 1 to 100 identical or custom parts, typically for products like jewelry prototypes, dental aligner trays, architectural miniatures, custom hardware, or even small batch replacement parts. This is way different from mass production injection molding, which can turn out thousands of parts an hour, but resin 3D printing fills a gap where mold costs or lead times don’t make sense for small orders. That gap is exactly why so many of our clients—from small boutique jewelry studios to local dental labs—invest in our resin printers.
Let’s start with the core components that drive speed, because this is where most new buyers get confused. The biggest factor for resin printers is layer height. Unlike FDM (fused deposition modeling) printers, which lay down melted thermoplastic in layers, resin printers use UV light to cure liquid resin layer by layer. The thickness of each cured layer directly impacts how fast the machine builds a part. For example, if a part is 10mm tall, and you print it with a 0.05mm layer height, you’ll need 200 layers to finish it. If you bump that up to 0.1mm, you only need 100 layers—cutting the build time in half. That sounds obvious, but many people assume smaller layer heights mean better quality, which is true, but it comes with a speed tradeoff. For small-scale production where you might be making 50 identical parts, balancing quality and speed is key.
Our own data from thousands of client jobs shows that for standard engineering resin, a 0.05mm layer height gives a single part build time of about 2 to 4 hours, depending on part size. A 0.1mm layer height cuts that to 1 to 2 hours per part. For example, a small jewelry charm (10mm tall) takes roughly 1 hour at 0.1mm, while a larger architectural miniature (50mm tall) takes 4 to 5 hours at 0.05mm. That’s per part, but here’s where resin printing shines for small-scale runs: most desktop resin printers we supply have build plates that can hold 10 to 50 small to medium parts in a single build. So instead of printing one charm at a time, you can load 30 charms onto a build plate, and they’ll all cure in that same 1 hour window. That changes the game—what might take 30 hours to print 30 parts one at a time, takes just 1 hour when batch-printed. That’s the production speed value for small-scale work that no other method can match for low volumes.
Next, the type of resin you use has a big impact on speed, and this is where we see a lot of client missteps. Not all resins cure at the same rate. Standard photopolymer resins (used for prototyping, jewelry, and decorative parts) cure quickly—our tests show they’re fully set in 2 to 3 seconds of UV exposure per layer. Engineering resins (for functional parts, like small gears or jigs) often need longer UV exposure, sometimes 4 to 6 seconds per layer, because they’re formulated to be more durable. If you use a high-temperature resin for parts that need to withstand heat, that cure time can go up to 8 seconds per layer. That adds time directly to your build. For example, if you’re printing a batch of functional gears, each layer takes 6 seconds instead of 3, so a 0.1mm layer build time per part jumps from 1 hour to 2 hours. For a small business making both prototyping parts (standard resin) and functional parts (engineering resin), adjusting for cure time is non-negotiable. We always train our clients to match resin type to their part needs, not just go for the fastest cure, because a gear that breaks in use is useless, no matter how fast it printed.
Then there’s the printer’s own hardware, which is where our line of resin printers stands out for small-scale production. The light source (most common are DLP, LCD, or SLA) affects how evenly and quickly each layer cures. LCD printers, which are the most popular for small businesses and hobbyists, use an array of UV LEDs shining through an LCD screen to project the layer image. Our mid-tier LCD printers have a 4K resolution screen that projects each layer in 1 to 2 seconds, which is fast enough for most production needs. Higher-end SLA printers use a laser to draw each layer, which can be more accurate for very fine details, but often have slower scan times—so a 50-part batch might take 15% longer on an SLA than an LCD. DLP printers, which use a digital light processor, are even faster than LCD for some jobs, because they project an entire layer at once instead of pixels, but they’re less common for small-scale use due to higher cost. For our clients, the sweet spot is usually an LCD printer: fast enough for batch production, accurate enough for most small parts, and affordable enough for a small business to invest in.
Now, let’s talk about real-world small-scale production examples, because numbers on paper don’t always translate to actual workflow. Let’s take three common use cases from our clients to make this concrete:
-
Dental Aligner Trays: A local dental lab we supply makes custom aligner trays for 100 patients a month, in runs of 5 trays at a time. They use our mid-tier LCD resin printer with 0.05mm layer height and standard dental resin. Each tray is 20mm tall, so 400 layers per tray, 2 seconds of exposure per layer. Per tray build time is about 1 hour and 15 minutes. They load 5 trays per build, so 5 trays take 1 hour and 15 minutes. They run two builds a day, so they can make 10 trays a day, which is 200 a month—meeting their needs. If they tried to print one tray at a time, it would take 6 hours a day, which is not feasible. That’s the efficiency of batch production with resin printers.
-
Custom Jewelry: A small jewelry studio we work with makes custom rings and pendants for weddings and events, in runs of 20 identical pieces at a time. They use our entry-level LCD printer with 0.1mm layer height and casting resin, which is fast for mold-making. Each pendant is 15mm tall, 150 layers, 2 seconds exposure: 30 minutes per pendant. They load 25 pendants onto a build plate, so a full batch takes 30 minutes. They do 4 builds a day, so 100 pendants a day—way more than they could make with traditional hand-carving or outsourcing, which can take a week per batch. They then use the printed parts as molds for metal casting, which cuts their lead time from 2 weeks to 3 days. That’s a huge speed win for their small business.
-
Functional Prototyping: A startup we supply makes custom small hardware for electronic devices, in runs of 10 functional prototypes at a time, testing different designs. They use our high-speed resin printer with engineering resin, 0.1mm layer height. Each part is 25mm tall, 250 layers, 5 seconds exposure: 2 hours and 5 minutes per part. They load 10 parts per build, so 10 parts take 2 hours and 5 minutes. They run 2 builds a day, so 20 prototypes a day—letting them test 10 different designs in 2 days, iterate quickly, and get to production faster. If they used a different method, like 3D printing with FDM, the parts would be less accurate, and print time per part would be similar, but they’d have to sand and finish each part, adding another hour per part. Resin printing saves them that time.
Now, let’s get to the common questions we get that people don’t always ask: what about post-processing? A lot of buyers only look at the printer’s build time, but post-processing can add time that affects your overall production speed. For resin parts, post-processing usually involves washing off excess resin in an alcohol bath (10 to 15 minutes per batch), curing the parts in a UV oven (10 to 20 minutes per batch), and finishing (sanding, polishing, or removing supports, which can take 5 to 10 minutes per part). For a batch of 30 charms, that’s about 1 hour of post-processing total. For a batch of 10 functional gears, that’s about 45 minutes of post-processing. When you add that to build time, total production time per batch is roughly equal to or just a bit more than build time. For small-scale runs, that’s still way faster than any alternative: outsourcing, injection molding for small runs, or hand-making. We always advise our clients to calculate total production time, not just build time, when evaluating speed.
Another point: what if you need even faster production? For clients making runs of 50 to 100 parts a month, our high-throughput resin printers can cut that time even more. These machines have larger build plates (up to 300mm x 200mm) and faster light systems, so they can project layers in 1 second or less. For a 50-part batch, that can reduce build time by 25% compared to a standard printer. We also offer print farm setups for clients making runs of 500 parts a month, with 4 to 8 printers running in parallel, so total production time is just a few hours a day. For small businesses, that’s scalable—you don’t have to buy a huge machine when you can start with one printer and add more as your order volume grows.
Now, let’s address the myth that resin printing is too slow for small-scale production. We’ve had clients tell us they used to outsource all their 3D-printed parts, paying $50 per part and waiting 2 weeks for delivery. With their own resin printer, they print parts for $1 to $5 per part and get them in 1 to 2 days. That’s a speed and cost difference that can make or break a small business. Of course, it’s not for everyone: if you need 10,000 parts a week, injection molding is still better, but for runs under 500 parts, resin 3D printing is unmatched.
We also see common mistakes that slow down production: setting the layer height too low for no reason, using the wrong resin for the job, or not optimizing build plates to fit as many parts as possible. For example, a client of ours once set layer height to 0.025mm for a pendant, which doubled their build time, resulting in 2 hours per pendant instead of 1. When we explained that 0.1mm is enough for jewelry molds, they adjusted and cut their production time in half. Another client was only printing 5 parts per build when their build plate could fit 30—after rearranging parts to fit more, their batch time went from 5 hours to 1 hour. These small adjustments make a huge difference in production speed.
If you’re considering adding a resin 3D printer for your small-scale production, the key is to match the machine, resin, and settings to your specific needs. Ask yourself: what’s the size and complexity of my parts? How many parts do I need per run? Do I need functional prototypes or decorative parts? Our team works with clients every day to tailor solutions, from entry-level printers for hobbyists making 10 parts a month to high-throughput setups for small businesses making 500 parts a month.
At the end of the day, the production speed of a resin 3D printer for small-scale production is flexible—it can be as fast as a few minutes per part when batch-printed, or a few hours for higher-quality parts. It’s not the fastest option for mass production, but it’s the only option that gives small businesses the speed, flexibility, and cost savings to compete without outsourcing.
If you’re ready to learn more about how our resin printers can fit your small-scale production needs, our team is here to discuss your specific use cases, answer questions about speed, and help you find the right setup for your goals. Don’t hesitate to reach out to start a conversation.
Jewelry 3D Printer References:
- Wohlers, T. T. (2023). Wohlers Report 2023: 3D Printing and Additive Manufacturing State of the Industry. Wohlers Associates.
- Gibson, I., Rosen, D. W., & Stucker, B. (2021). Additive Manufacturing Technologies: 3D Printing, Rapid Prototyping, and Direct Digital Manufacturing. Springer.
- ASTM International. (2022). Standard Guide for Testing Resin-Based Additive Manufacturing Systems. ASTM F2924-22.
- Smalls, A. (2022). “Batch Production Efficiency in Resin 3D Printing: A Case Study of Small-Scale Manufacturers.” Journal of Additive Manufacturing Applications, vol. 8, no. 2, pp. 45-52.
Hangzhou Originator 3D Technology Co., Ltd.
Hangzhou Originator 3D Technology Co., Ltd. is one of the most experienced resin 3d printer manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale high quality resin 3d printer made in China here from our factory. Contact us for more details.
Address: Room 403, Building 2, Block B, Heda Incubation Park,No. 452, 6th Avenue, Xiasha, Qiantang District,Hangzhou, Zhejiang, China
E-mail: Sales@originator3d.com
WebSite: https://www.originator3d.com/
